Menu
Monday
9:00-5:00
Tuesday
9:00-5:00
Wednesday
9:00-5:00
Thursday
9:00-5:00
Friday
9:00-5:00
Saturday
9:00-4:00
Sunday
CLOSED
For global buyers, quality is not secured by a final glance at finished goods. It is built through consistent checks across suppliers, production stages, packaging, documentation, and shipment preparation. This is where Tour-Level Quality Control becomes commercially important. It gives buyers a structured view of what happens beyond a single factory visit. A qualified inspector may review raw materials, compare samples with approved specifications, observe critical processes, and record measurable findings. Small details matter. A loose seam, uneven coating, incorrect label, or damaged carton can become an expensive problem after arrival.
W. Edwards Deming, one of the most influential quality-management experts, said, “Quality comes not from inspection, but from the improvement of the production process.” His principle remains highly relevant to international sourcing. Tour-Level Quality Control should not merely identify defects. It should reveal recurring causes, strengthen supplier communication, and support practical corrective actions. Clear photographs, lot numbers, inspection records, and acceptance criteria make decisions more reliable for buyers working across distance and time zones.
No control system catches everything. That limitation matters. Inspections can be rushed, samples can be imperfect, and specifications may remain unclear. Buyers should therefore combine field experience with documented procedures and realistic risk assessment. The strongest programs review patterns over time, not isolated failures. When quality information moves quickly from the production floor to the purchasing team, companies can respond earlier, protect customer expectations, and build more dependable global supply relationships. That is the real value of Tour-Level Quality Control: visibility before problems become commitments.
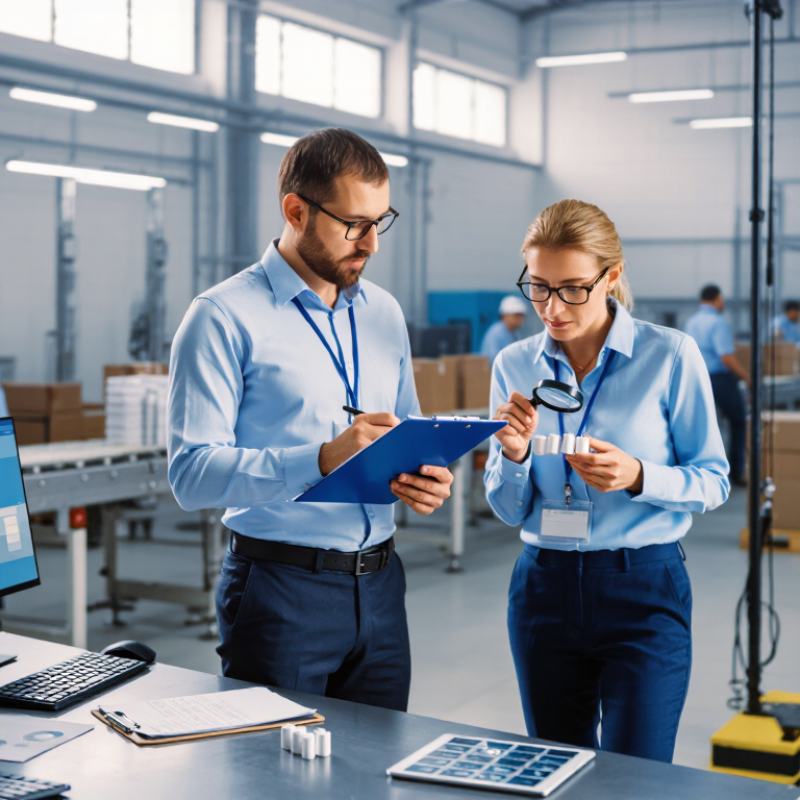
Tour-level quality control means checking manufacturing during planned factory visits, not only before shipment. For global buyers, quality is not proven by a final sample alone. It is verified across the production cycle. An experienced inspector may review incoming materials, observe cutting, and compare first-off units with approved specifications. Small deviations are easier to correct at this stage. A loose seam. A wrong coating thickness. These details can become expensive after shipment.
Effective control depends on a written inspection plan and consistent evidence. During each tour, trained personnel should record batch numbers, measurements, photos, and corrective actions. They should sample products through a defined method, rather than choosing only attractive pieces. Critical dimensions require calibrated tools. Records matter. Buyers can connect a defect to a process step, work shift, or material lot. Independent verification also reduces pressure on factory teams to hide weak results.
Tour-level control is not a perfect shield. An inspection can miss defects between samples, especially when production changes quickly. I have seen teams focus on appearance while overlooking compressed packaging or incorrect label placement. That is a useful warning. The checklist must reflect real delivery risks, not merely familiar factory routines. Buyers should review failed inspections, question weak controls, and adjust sampling when evidence changes. A carton opened at destination should match the report created on the factory floor.
Why Tour-Level Quality Control Matters for Global Buyers?
Why Consistent Quality Matters to International Buyers
International buyers need more than one attractive sample. They need every shipment to match the approved standard. A small color difference can affect an entire retail display. A loose thread can create returns across several markets.
Experienced quality teams check materials, dimensions, stitching, labeling, and packaging before shipment. They compare production goods with signed samples and clear tolerance sheets. Measurements should be recorded, not remembered. For example, a five-millimeter size difference may seem minor during inspection. It can become serious when products are packed together.
Details matter greatly.
Reliable control also requires checks at different production stages. An early inspection can find incorrect fabric or weak components. A final inspection can reveal carton damage, missing labels, or inconsistent quantities. Photos, inspection records, and corrective-action reports help buyers understand what happened. They also create accountability between factories, inspectors, and purchasing teams.
No production system is perfect. A careful team can still miss a shade variation under poor lighting. That weakness deserves review, not excuses. Better lighting, calibrated tools, and repeated training can reduce the risk. International buyers often work across time zones, so clear reports and prompt updates are equally important. Consistency builds confidence slowly, shipment by shipment, especially when quality expectations are understood before production begins.
| Quality Dimension | Measurable Indicator | Definition and Data Method | Required Evidence | Why It Matters to International Buyers |
|---|---|---|---|---|
| System Control Quality management system | Process conformity status | Verify whether documented procedures exist for purchasing, production, inspection, nonconformity control, corrective action, and continual improvement. | Quality manual, process procedures, internal audit records, management review records, and certification or conformity documentation where applicable. Reference: ISO 9001:2015. | Reduces dependence on individual operators and makes quality performance more repeatable across orders and production periods. |
| Incoming Control Material and component quality | Incoming acceptance rate | The percentage of incoming lots or batches accepted after inspection against approved specifications, drawings, certificates, and sample requirements. Accepted lots ÷ inspected lots × 100 | Incoming inspection reports, supplier certificates, material test reports, lot numbers, and quarantine or release records. | Prevents defective materials from entering production and lowers the risk of inconsistent finished goods. |
| Sampling Integrity Lot inspection | Sampling plan and acceptance number | A statistically defined sample size and acceptance or rejection rule selected according to lot size, inspection level, and the buyer’s agreed quality limit. | Inspection level, sample size, defect classification, acceptance number, rejection number, and signed inspection results. Reference: ISO 2859-1. | Creates a consistent inspection method instead of relying on subjective visual judgment or changing sample sizes. |
| Defect Prevention Product conformity | Defect rate by severity | Defects should be recorded separately as critical, major, or minor according to the approved product specification and risk assessment. Defect rate = recorded defects ÷ inspected units × 100 | Defect photographs, inspection checklists, defect classification rules, dimensional results, functional test records, and rework reports. | Helps buyers distinguish safety or functional risks from cosmetic issues and supports objective release decisions. |
| Measurement Control Calibration and traceability | Calibration validity | The percentage of measuring devices used for acceptance decisions that are within their calibration period and traceable to recognized measurement standards. Valid devices ÷ devices used × 100 | Equipment register, calibration certificates, identification labels, calibration due dates, and out-of-tolerance impact assessments. References: ISO 10012 and ISO/IEC 17025. | Ensures that dimensions, weights, temperatures, electrical values, and other test results are technically reliable. |
| Process Stability Production consistency | Process capability index | Cp and Cpk compare the natural variation of a stable process with the specification limits. The acceptance threshold must be defined by product risk and contract requirements. Cp = (USL − LSL) ÷ 6σ | Control charts, capability studies, measurement data, specification limits, process parameters, and documented reaction plans. | Identifies whether a process can repeatedly meet specifications before large quantities are produced. |
| Traceability Batch and lot control | Traceability coverage | The percentage of shipped units, cartons, or pallets that can be linked to a production date, production line, material lot, inspection record, and shipment record. Traceable units ÷ shipped units × 100 | Batch codes, carton labels, production records, material lot records, inspection reports, packing lists, and shipment references. | Enables faster containment, targeted recalls, and accurate investigation when a quality issue appears in a destination market. |
| Corrective Action Nonconformity closure | Corrective action closure rate | The percentage of corrective actions closed by the agreed due date after root-cause analysis, containment, implementation, and effectiveness verification. On-time closed actions ÷ due actions × 100 | Nonconformity reports, root-cause analysis, containment records, corrective action plans, verification results, and closure approvals. | Shows whether recurring defects are eliminated rather than repeatedly sorted, repaired, or accepted as a normal cost of doing business. |
| Shipment Release Pre-shipment verification | Final inspection pass status | A shipment is released only after quantity, appearance, dimensions, function, packaging, labeling, and required documents are checked against the approved order requirements. | Final inspection report, approved sample, order specification, packing list, label photographs, functional test records, and release authorization. | Prevents nonconforming products, incorrect quantities, and labeling errors from crossing borders and creating avoidable logistics costs. |
| Delivery Reliability On-time and in-full performance | OTIF percentage | Measures whether an order arrives by the agreed date and contains the complete confirmed quantity. Orders on time and complete ÷ total orders × 100 | Purchase order, confirmed delivery date, shipment documents, receiving records, shortage reports, and arrival date. | Connects quality control with inventory planning, customs clearance, production scheduling, and customer service performance. |
| Audit Governance Independent verification | Audit finding closure | The percentage of audit findings that have documented corrective actions implemented and verified as effective within the agreed timeframe. Verified closed findings ÷ total findings × 100 | Audit plan, auditor competence records, objective evidence, finding classification, corrective action records, and follow-up audit results. Reference: ISO 19011. | Provides confidence that quality controls are operating in practice, not only appearing in written procedures. |
Tour-level quality control turns a supplier visit into a documented decision process. A trained inspector checks production, materials, packaging, and records on site. The visit should begin with a clear inspection plan. It must define sampling levels, critical defects, tolerances, and approval rules. ISO’s 2023 Survey recorded more than 1.2 million ISO 9001 certificates worldwide. Yet certification alone cannot prove every shipment is consistent. Physical evidence still matters.
The process starts with supplier confirmation and production scheduling. Inspectors then verify raw materials against approved specifications. During production, they measure dimensions, observe workmanship, and photograph key findings. For finished goods, they use recognized sampling standards, such as ANSI/ASQ Z1.4. Results are recorded in a time-stamped report. Any failure should include corrective action, responsibility, and a deadline. ASQ quality-cost guidance notes that poor quality can consume 15–20% of sales. Early detection is usually cheaper. Not always, though. A rushed tour can miss hidden process weaknesses.
Tips: Ask inspectors to test high-risk features first. Compare samples with the approved reference unit. Require photos beside measuring tools. Review recurring defects across several tours, not one visit. Leave room for judgment; a checklist cannot replace experienced observation.
Tour-level quality control gives global buyers evidence before goods leave the factory. It turns a supplier promise into measurable checks. That difference matters. Experienced inspectors compare approved samples with finished units, not just paperwork. They verify dimensions, materials, color, labeling, workmanship, and packaging. Each result should match the buyer’s specification and destination requirements.
Sampling plans such as ISO 2859-1 help define inspection quantities and acceptable quality limits. Inspectors may use calibrated calipers, weighing scales, moisture meters, and electrical testers. Functional checks reveal problems that visual inspections miss. Drop tests can expose weak cartons. Seal tests can identify hidden leakage. Photos, serial numbers, and signed reports strengthen traceability. An independent laboratory may test materials when certificates alone seem insufficient.
Good control also includes corrective action. A failed batch should not simply be rechecked without examining its cause. Our early checklists sometimes focused too heavily on appearance. That was a weakness. Production records, worker instructions, and process changes can explain repeated defects. No inspection is perfect. Sampling can miss rare failures, especially when production changes late. Clear communication, calibrated tools, and an honest defect report help buyers make safer release decisions. 恒一
Global buyers rarely lose money from one visible defect. They lose it through repeated small failures: wrong labels, weak cartons, mixed batches, or late rework. Tour-level quality control turns these risks into evidence during production. An inspector can compare approved samples, measure dimensions, photograph packaging, and verify batch records before shipment. ASQ estimates poor quality may cost 15% to 20% of sales, with some operations reaching 40%. The figure is not universal. It is still uncomfortable.
A practical control plan reduces commercial uncertainty. Pre-production checks confirm materials and specifications. During-production checks catch drift while correction remains affordable. Final inspections verify quantity, function, labeling, and loading condition. ISO’s 2022 Survey recorded 1,265,216 ISO 9001 certificates across 188 countries and economies. Certification does not guarantee every shipment. It shows why documented processes and independent evidence matter. The WTO reports that full trade-facilitation implementation could reduce trade costs by 14.3%. Quality control supports that efficiency by preventing avoidable returns, delays, and disputes.
Tips: define critical-to-quality points in measurable terms; use approved samples; require timestamped photos; inspect high-risk changes; keep a corrective-action log; and review recurring defects monthly. Do not rely on a single final inspection. Sampling has blind spots. Supplier declarations can also be incomplete. A missed defect should trigger a process review, not only a refund request. Buyers should compare inspection findings with claims, delivery records, and customer complaints. That uncomfortable comparison often reveals where controls look strong but perform weakly.
